
How to Control Femtosecond Laser Drilling Taper
- Controlling femtosecond laser drilling taper depends on beam delivery strategy, dynamic focus control, beam shaping, and process parameters working together.
- The right taper type, positive, zero, or negative, depends on what the application needs, not on which option is more advanced.
- Material properties affect how tightly a given taper target can be held, so a specification proven on one material should not be assumed to transfer directly to another.
- Specifying taper clearly on a drawing and validating it through a feasibility study prevents mismatches between design intent and what a production process can actually hold.
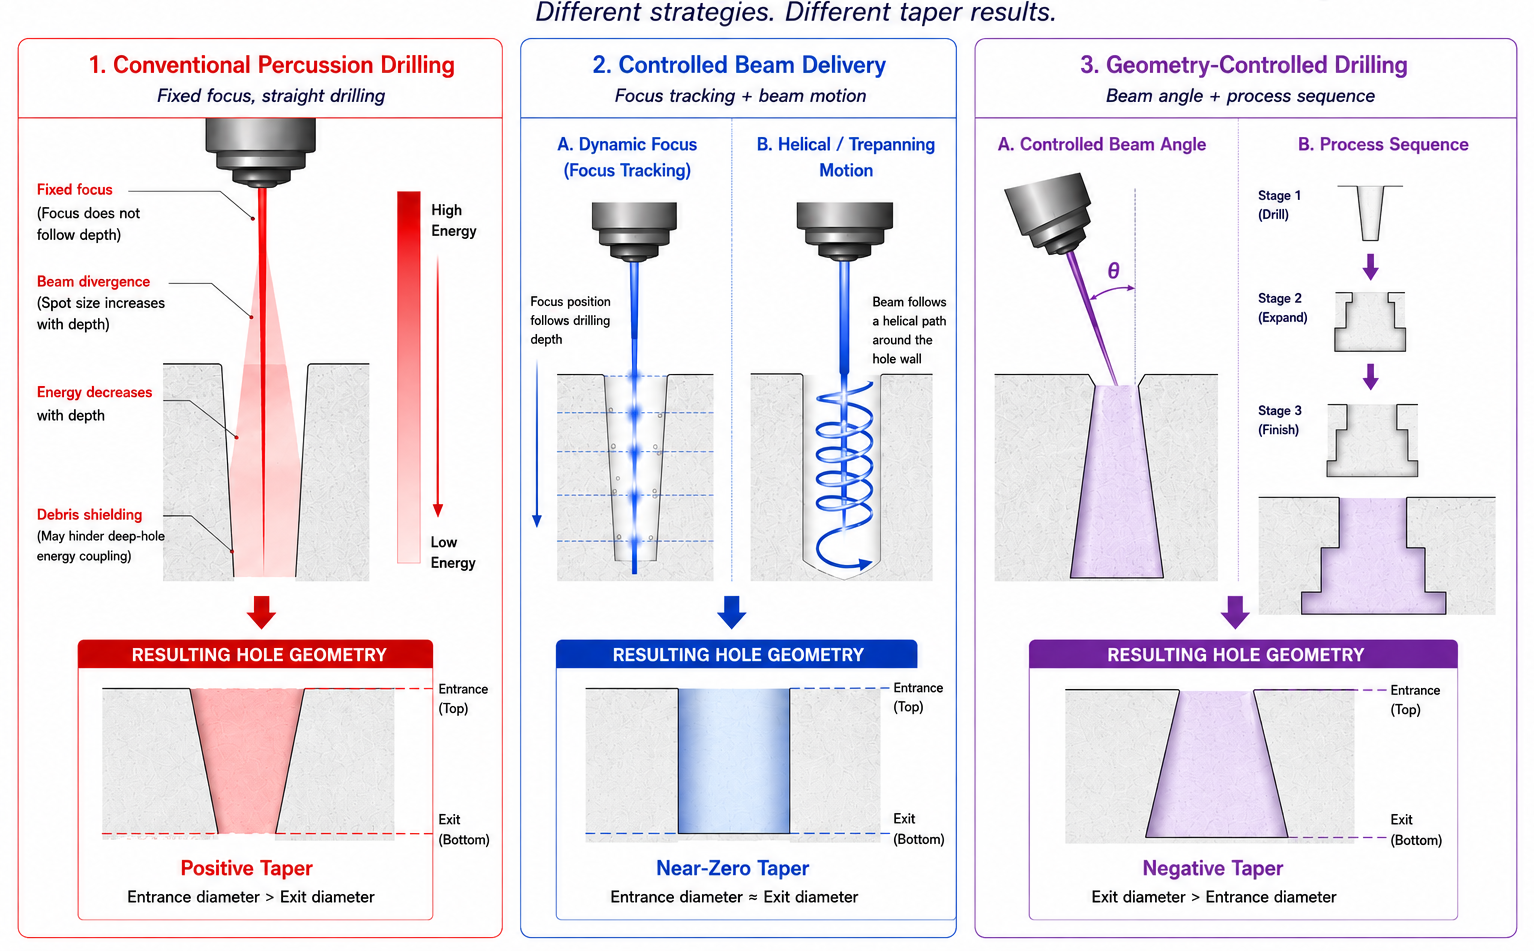
An engineer specifies a taper angle on a drawing, sends it to three laser drilling suppliers, and gets three different answers about whether it is achievable. That gap between a specification and a shop's real process capability is where most taper-related delays start. Hole taper falls into three categories: positive, where the entrance diameter is larger than the exit; zero, where the two are approximately equal; and negative, where the exit is larger than the entrance (see Part One for how and why each one forms). This guide covers how to control taper across all three geometries, how to choose the right type for an application, what changes by material, how to specify it on a drawing, and what a production-grade process actually looks like.
How to Control Hole Taper in Femtosecond Laser Drilling
Hole taper is mainly influenced by beam delivery, focal position, beam profile, and process parameters. Their relative importance shifts with hole depth: deeper holes give beam divergence and energy loss more room to compound.
Controlling taper, whichever direction it needs to go, comes down to four levers working together.
Beam delivery strategy. Straight percussion drilling offers the least control and defaults toward positive taper, particularly as hole depth increases. Helical drilling and trepanning, which move the beam along a scan path rather than firing at a fixed point, let engineers actively shape the taper result.
Dynamic focus control. Shifting the focal plane along the Z-axis as the hole deepens keeps the beam waist positioned where ablation is actually happening, instead of fixed at the entrance surface. This is one of the most direct ways to reduce taper in laser drilling of deep or high-aspect-ratio holes.
Beam shaping. Reshaping the beam profile toward a more uniform intensity distribution over a longer effective focal depth reduces the natural falloff in fluence between the entrance and the bottom of the hole. This works alongside dynamic focus rather than replacing it.
Process parameters. Pulse energy, repetition rate, scan speed, and number of passes all influence how much material is removed at each depth increment. Small adjustments here fine-tune a result that is already in the right range; they rarely fix a process that is fundamentally mispositioned.
Micro hole taper control also depends on closing the loop with inspection. Measuring entrance and exit diameters with confocal microscopy or optical metrology after each process iteration is what turns a taper target into a repeatable production spec, rather than a one-off result on a single test part.
Which Taper Type Should You Choose for Your Application?
The right taper geometry depends on what the hole needs to do, not on which option sounds most advanced. This is where micro hole taper control becomes an application decision, not just a manufacturing capability.
Zero taper micro holes are the right call whenever a pin, probe, or fiber needs to seat consistently at any point along the hole's depth, or when a fluid or gas needs to pass through a bore without a changing cross-section. Probe card guide plates, precision dowel holes, and some optical apertures fall into this category.
Positive taper is often perfectly acceptable, and sometimes preferable, when a hole functions more like a funnel: fastener countersinks, self-aligning locating features. A slightly larger entrance simplifies assembly in these cases, and the exit diameter tolerance is the one that actually matters functionally.
Negative taper earns its place in flow and retention applications: nozzle orifices that need a wider internal chamber for spray or flow shaping, or features where a reverse-tapered bore helps lock a component or fill material in place.
| Taper Type | Typical Priority | Common Applications |
|---|---|---|
| Positive | Assembly ease, entrance-side tolerance | Countersinks, self-centering features |
| Zero | Consistent bore diameter through full depth | Probe card guide plates, alignment holes, optical apertures |
| Negative | Exit-side geometry, flow or retention function | Nozzle orifices, flow control components, retention features |
For femtosecond laser micro drilling specifically, all three are achievable on the same class of equipment, though each geometry needs its own process development for a given material and diameter range. The deciding factor is almost always the application, not a limitation of the process.
Material Considerations for Femtosecond Laser Drilling
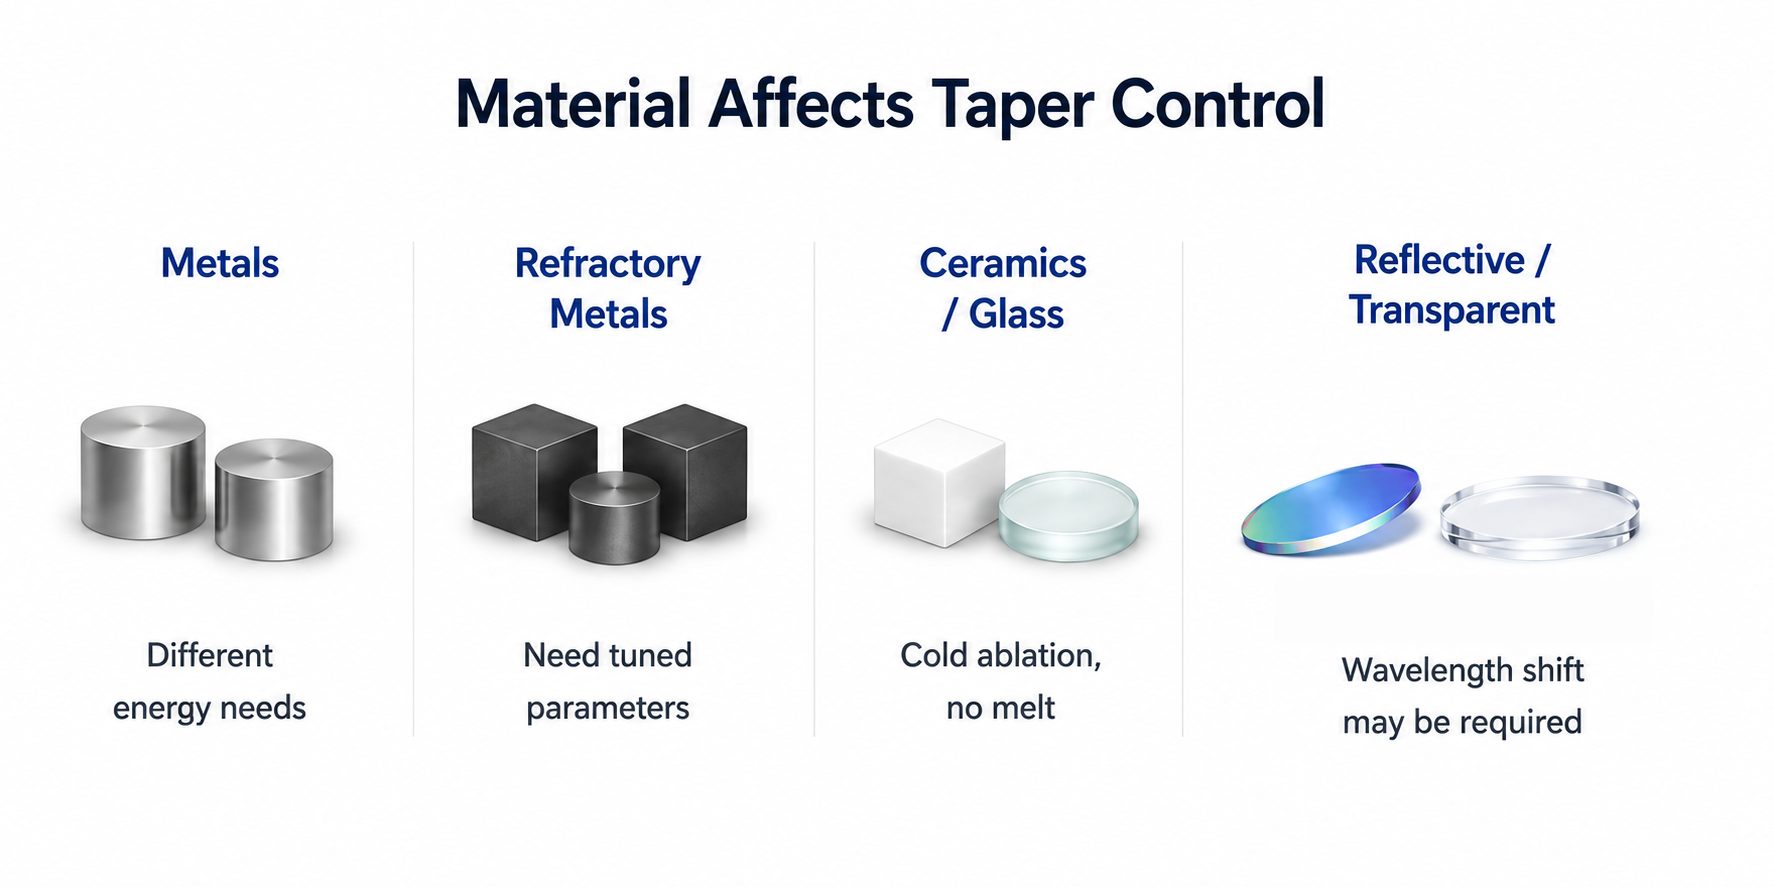
Material does not simply determine whether taper is possible. It determines the process window available for controlling it, because ablation threshold, thermal conductivity, and optical absorption all vary by substrate.
Metals such as stainless steel, titanium, and nickel alloys ablate cleanly under femtosecond pulses but differ in how much energy each requires, affecting how tightly a taper target can be held at depth. Refractory metals like molybdenum and tungsten, in particular, need carefully tuned parameters to avoid inconsistent hole walls at high aspect ratios.
Hard, brittle materials, including technical ceramics and glass, respond well to femtosecond cold ablation, since there is no melt phase to introduce microcracks. Their hardness, however, can narrow the process window for hitting a specific taper angle consistently.
Highly reflective or highly transparent materials sometimes require a shift in laser wavelength, from infrared toward green or ultraviolet, to reach a clean ablation threshold. Skipping this step can produce inconsistent taper simply because the beam is not coupling into the material efficiently in the first place.
None of this changes the underlying taper mechanics. It does mean the achievable process window shifts by material, so a taper specification validated on one material and thickness should not be assumed to transfer directly to a different one without a short process check.
How to Specify Laser-Drilled Hole Taper on a Drawing
Don't specify taper with a single angle callout alone. Taper is easy to specify ambiguously and hard to inspect ambiguously, so drawings benefit from redundancy.
The most reliable approach combines three values: entrance diameter with tolerance, exit diameter with tolerance, and the material thickness the tolerance applies across. This removes any question about which reference axis or plane a taper angle callout is measured from, which matters more than it sounds like it should once tolerances get into single-digit micron territory.
A taper angle callout, calculated as θ = arctan[(entrance diameter − exit diameter) / (2 × depth)], can be added alongside the diameter tolerances for clarity, but it should not replace them. Two holes with the same taper angle can still fail a fit-up check if their absolute diameters land at opposite ends of a tolerance band.
For depth-to-diameter ratios above roughly 5:1, it is worth flagging the taper requirement explicitly, rather than assuming a standard drilling process will hit it by default. High-aspect-ratio holes are exactly where uncontrolled positive taper becomes most visible. Before finalizing tight taper tolerances on a drawing, a short feasibility study against the actual material, thickness, and diameter range is the fastest way to confirm the spec is achievable, rather than discovering a mismatch after parts are already in production.
MONO Femtosecond Laser Machining Capability
MONO's femtosecond laser platforms are built specifically around the kind of taper control this guide describes, not adapted from a general-purpose cutting system.
Standard processing capability includes straight holes, taper holes, countersinks, and composite hole geometries, with positioning accuracy to ±1 μm on the X, Y, and Z axes and taper control precision to ±1 μm. Hole diameters from 0.02 mm to 2.5 mm are supported, with depth-to-diameter ratios up to 12:1 as a standard capability and higher ratios achievable with process optimization. Every order is verified using non-contact optical metrology and confocal microscopy to confirm entrance and exit geometry, taper angle, and wall roughness against the drawing before parts ship.
Equipment includes the ML-VORTEX femtosecond laser trepanning center, purpose-built for zero-taper and negative-taper micromachining, alongside 5-axis systems for complex micro-drilling geometries. Materials in regular production include stainless steel, titanium, nickel alloys, molybdenum, tungsten, technical ceramics, and glass.
MONO operates under ISO 9001:2015, ISO 14001:2015, and ISO 45001:2018 certification, with UDEM conformity assessment under the EU Machinery Directive 2006/42/EC. The R&D team, making up roughly 60% of staff with more than 10 years of femtosecond laser process experience, has addressed more than 2,000 precision manufacturing requirements from clients across aerospace, semiconductor, watchmaking, and advanced materials sectors.
Conclusion
Hole taper is not a single problem to eliminate. It is a geometric parameter, positive, zero, or negative, that should be chosen deliberately based on what a hole needs to do once the part is in service. Femtosecond laser drilling taper control gives engineers that choice: cold ablation produces clean, geometrically consistent hole walls, and multi-axis beam delivery, dynamic focus control, and beam shaping let taper be treated as a controllable process parameter rather than an incidental side effect, one that can be measured and validated against a drawing requirement. Whether a project calls for a straight zero-taper bore, a functional positive taper, or a deliberately engineered negative taper, the right starting point is confirming what the application actually requires, then validating that target against the real material and geometry before finalizing a drawing.
FAQ
Q1. Does taper control slow production?
Some, but not in proportion to the precision gained. Dynamic focus control and beam shaping add processing steps compared to straight percussion drilling, but on established platforms, the added cycle time is usually the smaller cost next to reworking or scrapping parts that miss a functional taper spec.
Q2. Which materials are more difficult for tight taper control?
Materials with challenging optical coupling, high reflectivity, high transparency at the selected wavelength, or narrow process windows can require more process development to hold a tight taper specification.
Q3. Is a taper angle callout enough?
No. A single taper angle can be satisfied by more than one combination of entrance and exit diameter, so two parts with an identical callout can still fail a fit-up check. Specifying entrance diameter, exit diameter, and material thickness together removes that ambiguity.
Q4. Does a nozzle always need negative taper?
No. The required geometry depends on the flow path and spray function. Negative taper can be useful where an enlarged internal section is part of the flow design, while zero or positive taper may be appropriate for other nozzle geometries.
Q5. Does switching taper types need new tooling?
Not new tooling, a different process. The same multi-axis trepanning hardware handles zero and negative taper by adjusting incidence angle and focal position differently, so switching between them is a process change, not an equipment change.